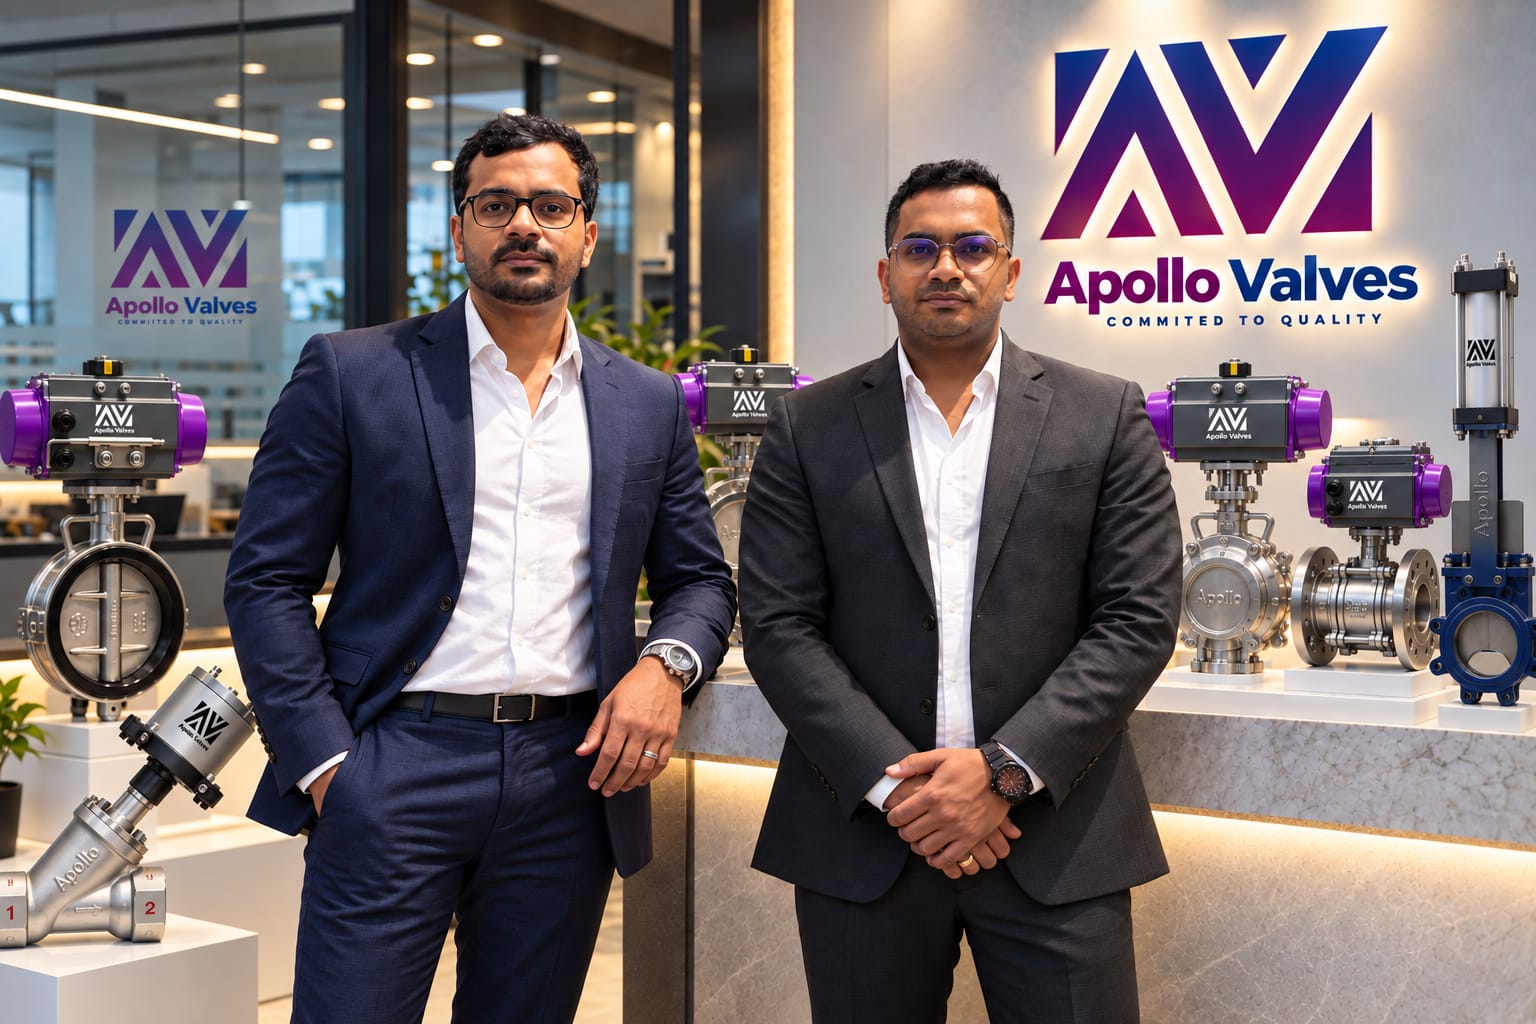
From a focused manufacturing facility in Bhosari MIDC, Pune, Apollo India Valves has grown into a comprehensive industrial valve supplier trusted by some of India's largest process industries.
Apollo India Valves was established with a clear purpose: to provide Indian industries with access to world-class industrial valve solutions without compromise on quality, delivery or after-sales support. Operating from our dedicated facility in C Line J 514, MIDC Bhosari, Pune, we manufacture and supply a comprehensive range of valve types across multiple material classes and actuation modes.
Our production covers ball valves, butterfly valves, gate valves, globe valves, knife gate valves, check valves, control valves, Y-strainers, triple offset butterfly valves, trunnion ball valves, solenoid valves, PFA lined valves, pharma valves and PP valves — in manual, pneumatic actuated and electric motorized configurations.
Our products serve a wide spectrum of applications including Oil & Gas, Power Generation, Mining, Chemical Process, Marine, Pharmaceutical, Textile, Food & Beverage, Water Treatment and general industrial markets across India and export markets.

Our journey in the valve industry began with a simple dream — to learn, grow, and build something of our own. Starting from the basics, we learned the industry and understood what customers truly needed.
Quality, reliability, and commitment became the foundation of every relationship we built. The journey came with challenges, setbacks, and failures — but every experience taught us something new.
Every order built our confidence. Every challenge made us stronger. Every customer's trust became part of our growth story and pushed us to do more, build better, and never settle.
Apollo India Valves now manufactures pneumatic, manual, and electrically operated valves, serving diverse industrial requirements across India and international markets.
2013 was where our journey began. Today, that journey has a name —
APOLLO INDIA VALVES.
And we are still building, growing, and moving forward.
Every single valve that carries the Apollo name passes through a rigorous multi-stage quality verification process before it leaves our facility.
100% body pressure testing to verify structural integrity of every valve housing before dispatch.
Seat seal verification at rated pressure to ensure zero-leakage performance throughout the valve's service life.
Operational torque verification ensures correct actuator sizing and smooth valve cycling under load conditions.
X-ray inspection of cast components to detect sub-surface porosity, inclusions and casting defects non-destructively.
MPI testing to identify surface and near-surface discontinuities in ferromagnetic valve components.
Thickness measurement and internal flaw detection across valve body walls and critical pressure-retaining parts.
PMI verification confirms the exact alloy composition of materials — critical for corrosion-sensitive applications.
Surface crack detection using liquid penetrant on non-ferromagnetic and stainless steel valve components.
Our valve solutions are engineered and tested to perform in the world's most demanding industrial environments.