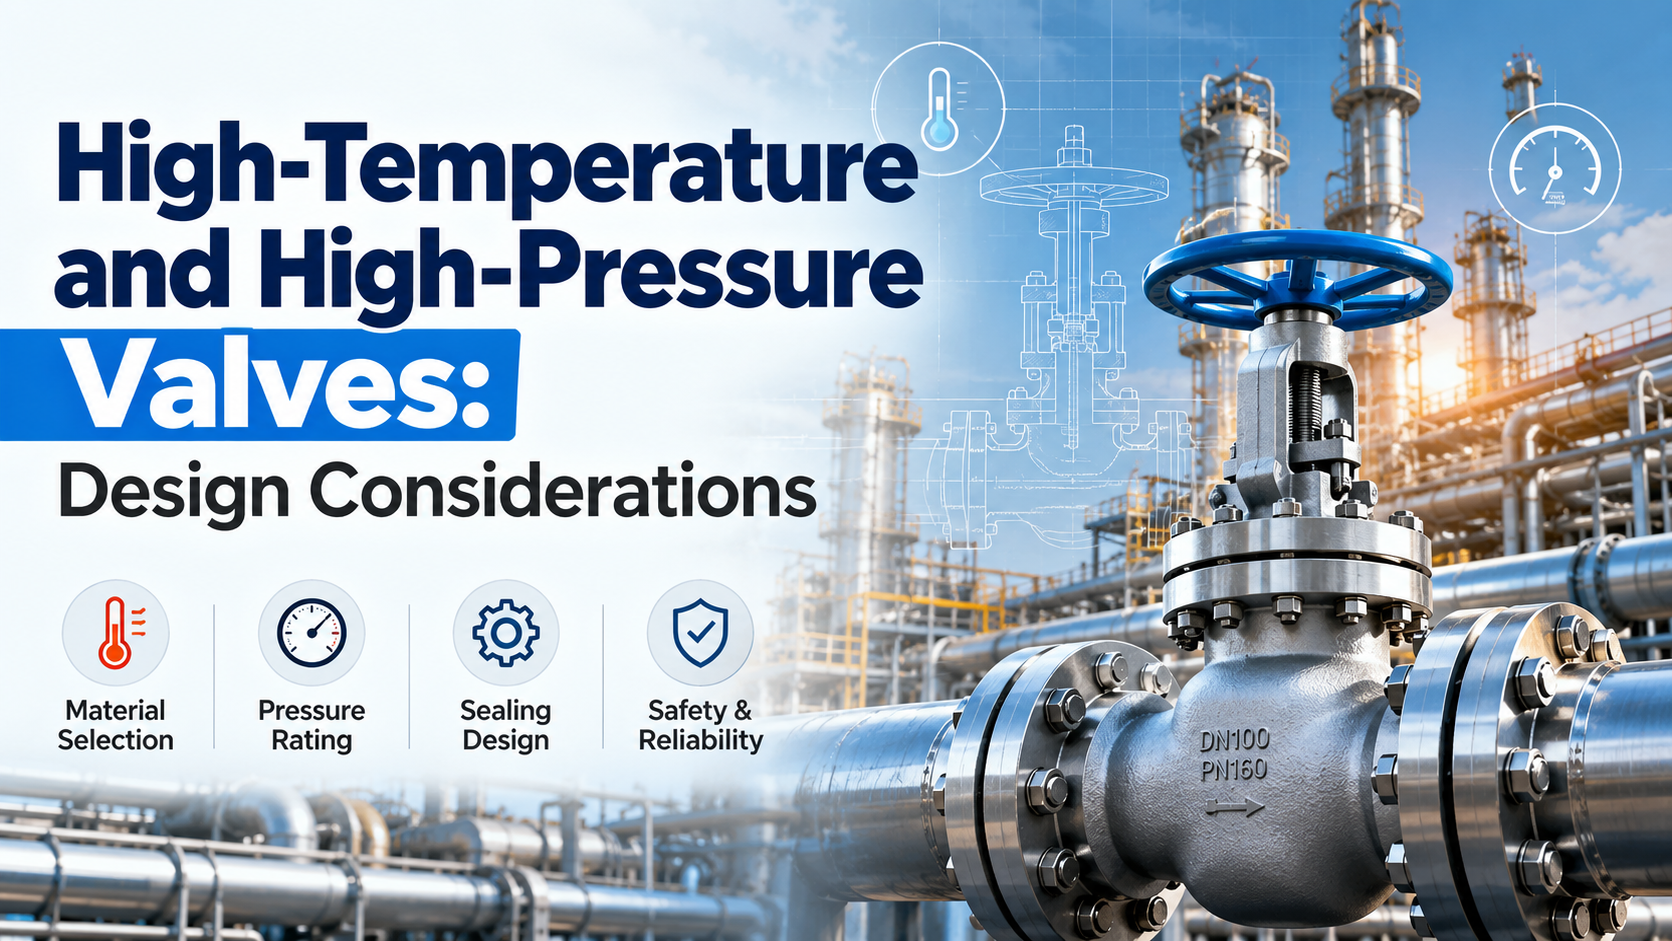
A valve that works perfectly on a cooling water line can fail within months on a 540°C main steam header. Heat and pressure change everything: how metal behaves, how seals hold, and how the valve body moves as the plant heats up and cools down.
In power plants, refineries, petrochemical units and process boilers, these valves sit on the lines where a leak is not an inconvenience. It is a shutdown, a safety incident, or both. That is why high-temperature and high-pressure (HTHP) valves are engineered differently from general-purpose valves.
This guide walks through the design considerations that matter most, written for plant engineers, maintenance heads and procurement teams who want to specify the right valve the first time.
What Makes High-Temperature, High-Pressure Service Different?
HTHP service is any application where temperature, pressure or both push a valve close to the limits of standard materials and seals. In practice, that usually means steam above 400°C, pressure classes of ASME 900 and above, or both together.
Three things happen in these conditions that do not happen on ordinary lines:
Metal loses strength as it heats up. A carbon steel body rated for a certain pressure at room temperature can safely hold far less at 450°C. This is why every pressure class has a pressure-temperature rating table, not a single number.
Creep sets in. Above roughly 425°C, steel slowly deforms under constant load over months and years. A valve that passes its hydro test can still distort in service if the material is wrong.
Thermal cycling stresses every joint. Each start-up and shutdown expands and contracts the body, bonnet, stem and bolting at different rates. Seals and gaskets must survive thousands of these cycles.
Good HTHP valve design is really about managing these three effects.
1. Material Selection: Start with the Operating Temperature
Material choice is the single most important decision in HTHP valve design. Get it wrong and nothing else will save the valve.
These ranges are guidelines; the final limit always comes from ASME B16.34 tables and the plant's design code.
The trim matters as much as the body. Seats and wedge faces in HTHP valves are usually hardfaced with Stellite (cobalt-chrome alloy). It resists galling and erosion at temperatures where plain stainless steel trim would wear quickly. Stems are typically 410 stainless steel or precipitation-hardened grades for strength at heat.
Bolting is often overlooked. B7 studs lose strength above around 450°C, so high-temperature valves move to B16 bolting, and the hardest services use alloy or nickel-based fasteners.
2. Pressure Class and Body Design
Pressure class (ASME Class 150 up to 2500, and 4500 for special cases) defines wall thickness, flange dimensions and the pressure the valve can hold at each temperature. For HTHP lines, classes 900, 1500 and 2500 are common.
A few body design points separate a reliable HTHP valve from a marginal one:
Adequate wall thickness per ASME B16.34, with extra allowance where erosion or corrosion is expected.
Smooth internal contours. Sharp corners concentrate stress and become crack initiation points under thermal cycling.
Butt-weld ends for high classes. Flanged joints are a leak path at high temperature; butt-weld ends remove that risk and are standard on most main steam lines.
Forged bodies for small bores. For sizes up to 2 inches, forged valves (API 602 style) offer denser, defect-free material compared with castings.
3. Bonnet Design and Thermal Expansion
The body-bonnet joint is where many high-pressure valves leak. Three bonnet types are common:
The pressure seal bonnet is the preferred design for HTHP service. The higher the line pressure, the tighter the seal becomes, which is exactly the opposite of a bolted joint, where pressure tries to push the bonnet off.
Thermal expansion needs equal attention. Gate valves in hot service can suffer thermal binding: the wedge is closed while hot, the body cools and contracts, and the wedge becomes jammed. A flexible wedge design absorbs this movement and is standard for steam service.
A related problem is pressure locking, where fluid trapped in the bonnet cavity heats up and pressurises, making the valve impossible to open. A cavity pressure relief hole or an external bypass solves it, and should be specified wherever the risk exists.
4. Sealing, Seats and Gland Packing
Even a perfectly designed body is useless if it leaks through the stem or the seat.
Gland packing: PTFE packing, common on low-temperature valves, degrades above roughly 230°C. HTHP valves use die-formed flexible graphite rings, often with braided graphite anti-extrusion rings at each end. Live-loaded packing (disc springs on the gland bolts) keeps compression steady through thermal cycles and cuts fugitive emissions. Packing tested to API 622 and valves qualified to API 624 are now a common specification in refineries.
Seats: Metal-to-metal seating with Stellite hardfacing is the norm. Soft seats are rarely suitable above 200–250°C.
Gaskets: Spiral-wound gaskets with graphite filler, or ring-type joints (RTJ) for high classes, handle temperature and pressure far better than compressed fibre gaskets.
Backseat: A good backseat lets the gland be inspected with the valve open and under pressure. It is a useful safety feature, though it should never replace proper isolation for repacking.
5. Choosing the Right Valve Type for HTHP Service
Not every valve type handles heat and pressure equally well.
For Indian boiler applications, valves on steam lines also need approval under the Indian Boiler Regulations (IBR). Asking for IBR-certified valves at the enquiry stage avoids delays at commissioning.
6. Testing and Standards That Matter
A well-designed HTHP valve is only as good as its testing. Key standards to call out in a purchase specification:
ASME B16.34: pressure-temperature ratings, wall thickness and design rules.
API 600 / API 602: cast and forged steel gate valves.
API 598 / ISO 5208: shell, seat and backseat pressure testing.
API 622 / API 624: fugitive emission testing for packing and valves.
IBR: mandatory for boiler steam lines in India.
For critical service, ask for non-destructive examination of castings (radiography, magnetic particle or dye penetrant testing), positive material identification (PMI) of body and trim, and full material test certificates traceable to the heat number.
7. Maintenance Tips That Extend Valve Life
Even the best valve needs care. A few habits make a real difference:
Warm up lines gradually. Sudden temperature changes are the fastest way to crack bodies and distort seats.
Retorque gland and bonnet bolts after the first heat cycle, as recommended by the manufacturer.
Do not use isolation gate valves for throttling. Partial opening erodes the seats quickly.
Inspect high-cycle valves at every planned shutdown, focusing on packing, seats and pressure seal rings.
Keep spare packing sets and seal rings of the correct grade in stock.
Designing a valve for high temperature and high pressure comes down to a handful of decisions made well: the right material for the temperature, a body and bonnet built for the pressure class, sealing that survives thermal cycling, and testing that proves it all before installation. Cutting corners on any one of them shows up later as leaks, stuck valves and unplanned shutdowns.
If you are specifying valves for steam, power, refinery or process service and want a partner who understands these trade-offs, talk to the engineering team at Apollo India Valves. Explore the full range of industrial gate, globe, check and ball valves at https://www.apolloindiavalves.com/ and share your operating conditions for a valve recommendation built around your application.